Stacked Against You: Specifying Recycled Corrugated for the Load It Actually Carries
The drop-in assumption that keeps costing buyers money
When a procurement team replaces a virgin-fiber corrugated box with a recycled-content equivalent, the swap usually happens on paper: same footprint, same flute, same "200 lb test" stamp on the Box Maker's Certificate, and a lower landed cost per unit. The assumption underneath the swap is parity. In practice, parity holds only for the conditions in which the original specification was validated — and those conditions are almost never the conditions in the buyer's warehouse.
Recycled linerboard is not inherently inferior. Mills have spent more than a decade engineering around the shorter fibers in old corrugated containers, and many recycled sheets now carry edge crush values that rival mixed virgin grades. The problem is that buyers tend to purchase recycled board on the same dimensional and grade shorthand they used for virgin stock, and that shorthand says very little about how a finished box behaves when it is stacked eight high for eleven weeks in a facility where relative humidity climbs past 75 percent each July.
What ECT measures, and what it quietly ignores
Edge crush test, run to TAPPI T811 and conditioned to TAPPI T402 standards — 73°F and 50 percent relative humidity — describes a board's resistance to a compressive force applied to its edges. It is a good proxy for stacking performance, and it is the basis for the McKee formula that converters use to estimate box compression strength. It is not, however, a measurement of the finished box.
Two distinctions matter for procurement. First, ECT is a board test; box compression test (BCT), run to ASTM D642, is the assembly test, and it captures the effects of scoring, fluting damage at the score lines, hand holes, and panel dimensions. A board that hits its ECT target can still produce a box that misses its BCT target by a wide margin. Second, Mullen burst — the familiar "test" number on many legacy specifications — measures resistance to puncture, not to sustained vertical load. Burst remains relevant where carrier classification rules require it, but it is a poor predictor of whether a stack will survive a long dwell in a humid facility.
Buyers should also note that the conditioning standard is doing a great deal of work. Board tested at 50 percent relative humidity and board sitting in a coastal Georgia warehouse in August are not the same material. Fiber absorbs moisture, hydrogen bonds loosen, and compression strength can fall substantially — published ranges commonly cited in packaging engineering run from 20 to 40 percent losses as humidity rises toward saturation. A specification written without a humidity assumption is a specification written for a laboratory.
Time is a load, too
Compression strength is not a static property. Under sustained load, corrugated creeps: the box deforms slowly and progressively, and the rate accelerates with moisture and temperature. Packaging engineers typically apply a safety factor of three to five when translating BCT into a working stacking load for short-term distribution, and that factor climbs for longer storage, taller stacks, pallet overhang, and uneven pallet patterns.
Procurement teams rarely see these calculations. They see a unit price and a box certificate. Closing that gap is the single highest-value change a buying group can make in a corrugated program: define the load case explicitly, in writing, and require the supplier to demonstrate performance against it.
A specification checklist for real distribution conditions
- Specify at the box level, not the board level. Require BCT data at the stack height and load actually used, in addition to ECT.
- State the conditioning protocol. Name the test method and the relative humidity at which results must be reported, including an elevated-humidity run that reflects the facility's worst season.
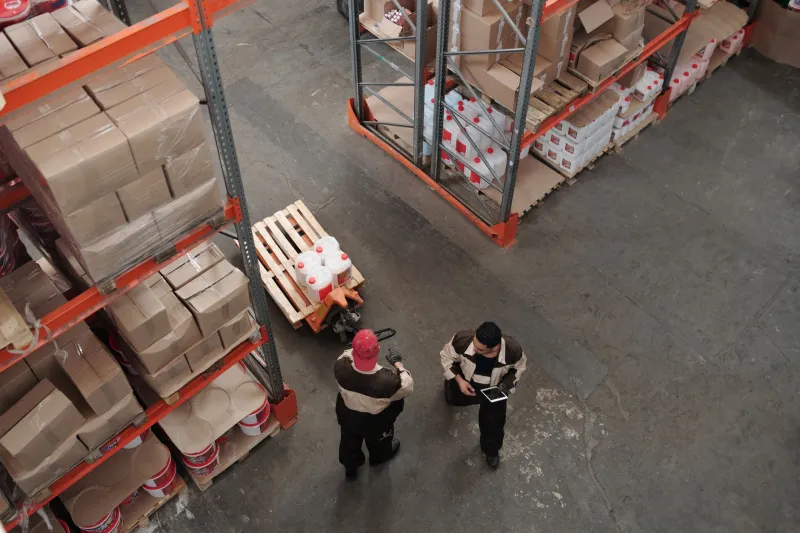
- Quantify the load case. Stack height, pallet pattern, overhang allowance, expected dwell time in the DC, and the humidity and temperature range the box will see.
- Require basis weight and flute profile on the certificate. Recycled board frequently compensates for shorter fiber with higher basis weight; buyers should know where the strength is coming from.
- Ask for creep or sustained-load data if dwell exceeds roughly 30 days, or if product value makes failure expensive.
- Validate with a real pallet, not a sample box. A compression test on a single box under a platen systematically flatters the design.
- Align with freight classification. Confirm the box meets the carrier rule it is shipped under, and that the certificate matches the construction actually supplied.
- Audit off the line. Pull boxes from production runs, not from the sample room.
- Write change control into the contract. Any shift in liner source, mill, or flute profile should trigger re-testing.
- Track damage rates by SKU. Field data is the ultimate check on whether the specification is right.
Questions that separate durable packaging from paper-thin claims
Ask the converter: Which mill supplies the recycled liner, and has it changed in the last twelve months? What BCT value does this box deliver at 80 percent relative humidity, and how was it measured? What safety factor did you apply against our stated stack load? Can you show creep data beyond 30 days? How does the score line affect compression in this dimension? What is the recycled content by weight, and is it certified or self-declared? Who ran the test, and can we see the report?
Suppliers with genuine engineering depth answer these quickly. Suppliers selling on price alone change the subject to lead times.
Reframing the cost conversation
The productive metric is not cost per box. It is cost per unit of protected product delivered — incorporating damage rates, replacement shipments, customer complaints, and the labor spent reworking crushed cases. A lighter, cheaper box that fails at the fourth pallet position is not a saving; it is a deferred expense with interest.
Recycled corrugated belongs in a serious circular procurement program. It simply deserves a specification written for the warehouse it will live in, rather than the laboratory it was tested in.